An integration engineer once spent three weeks troubleshooting a vision-guided robotic cell that kept rejecting good parts. The camera, mounted above a conveyor of anodized aluminum brackets, produced images so washed out by specular glare that the edge-detection algorithm could not distinguish a scratch from a reflection. Lighting adjustments helped marginally. Repositioning the camera helped a little more. The fix that finally solved the problem was a polarization filter threaded onto the front of the lens, which cut the glare enough for the algorithm to see the part rather than the light bouncing off it.
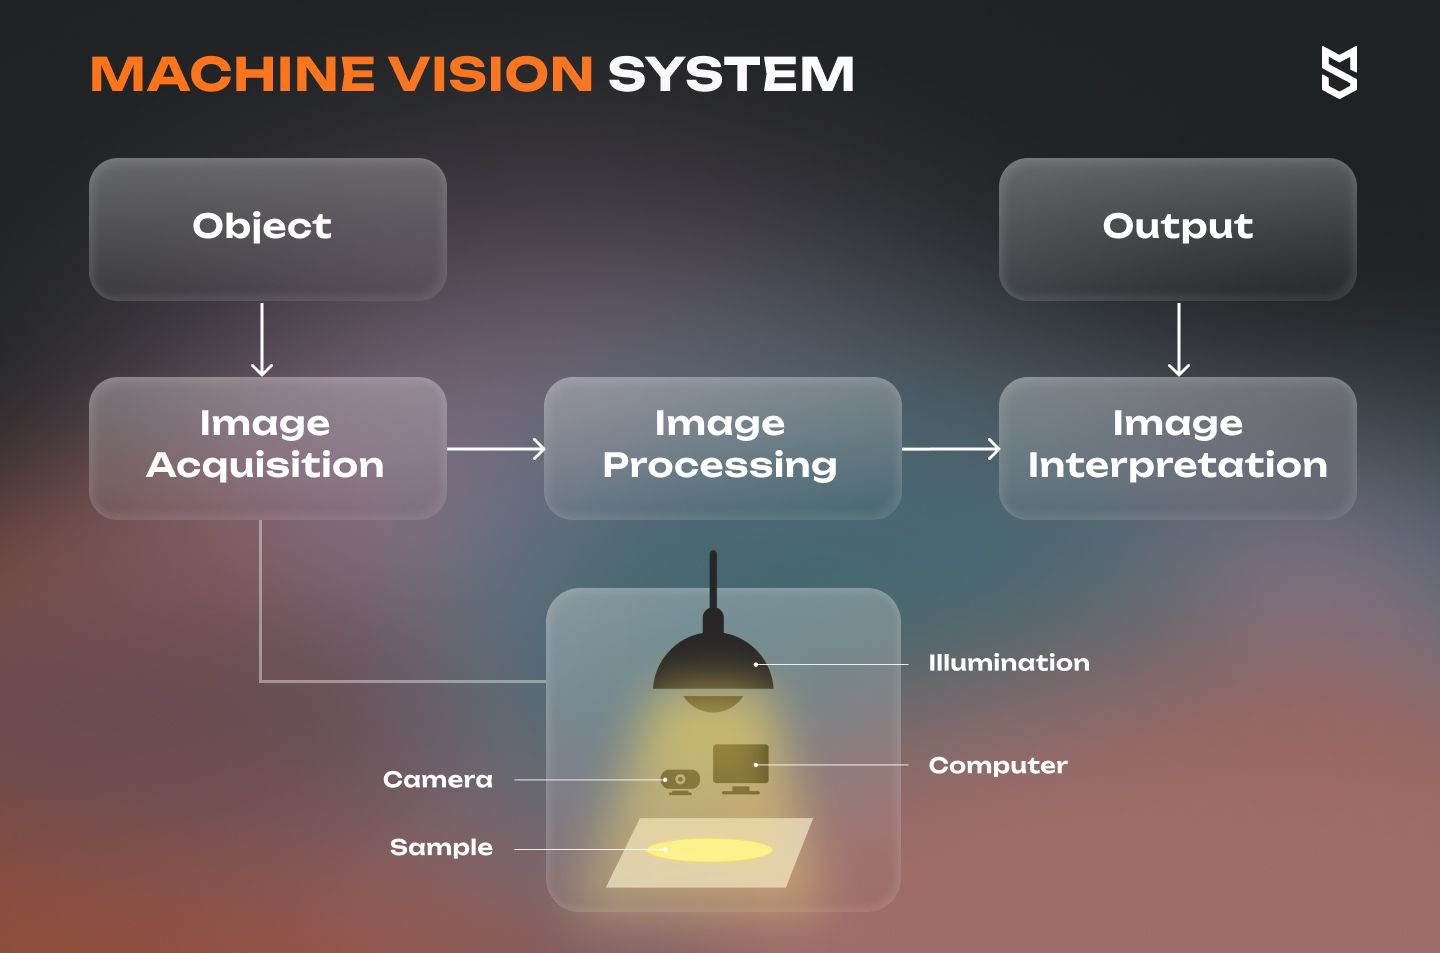
That anecdote captures a recurring challenge across factory automation: machine vision cameras are only as good as the light they receive, and reflective surfaces are everywhere in modern manufacturing. Metal stamping, glass assembly, painted automotive panels, and plastic injection-molded housings all generate reflections that can overwhelm sensor dynamic range. Polarization filters address this at the optical level, before a single pixel is processed, which makes them one of the more cost-effective upgrades available to system integrators working with demanding materials. machine Vision Lenses
This article examines how polarization filters function within machine vision lenses, where they deliver the clearest return on investment, and what trade-offs engineers should weigh before specifying them into a production line.
How Do Polarization Filters Actually Work in Optical Systems?
Light reflecting off a non-metallic surface becomes partially polarized, meaning its electromagnetic waves oscillate in a preferred orientation rather than randomly in all directions. A polarization filter contains a microscopic grid or film structure that blocks light waves oscillating outside a specific axis while allowing aligned waves to pass through. When mounted correctly in front of a lens and rotated to the optimal angle, the filter can suppress a substantial portion of the glare coming from a glossy surface while leaving diffusely scattered light largely unaffected. The result is an image with restored contrast and revealed surface detail that would otherwise be buried under a bright reflective wash.
This selective blocking is not magic; it follows Brewster's angle physics, where reflected light reaches maximum polarization at a specific angle relative to the surface normal, typically somewhere between 30 and 40 degrees for most industrial materials like glass, coated metals, and plastics. Engineers who understand this relationship can position cameras and lights deliberately to maximize the filter's effect rather than relying on trial and error. A filter mounted at the wrong rotational index, even a high-quality one, will underperform relative to a correctly indexed unit costing less.
Where Do Polarization Filters Deliver the Clearest ROI on the Factory Floor?
Automotive assembly lines inspecting painted body panels represent one of the most common deployment scenarios, since clear-coat finishes generate intense specular highlights under the ring lights typically used for defect detection. Semiconductor and electronics manufacturers rely on polarization control when imaging solder joints, glass substrates, and reflective solder paste, where even minor glare can mask a cold joint or a bridging defect. Food and beverage packaging lines inspecting shrink-wrapped or glass-bottled products also benefit substantially, because plastic film and glass are both aggressive specular reflectors under standard LED illumination. ClearView Systems
Metal part inspection is arguably the strongest use case. Machined aluminum, stainless steel, and chrome-plated components reflect light almost like mirrors, and without polarization control, a vision system may see nothing but a blown-out highlight where the actual feature of interest sits. In these settings, engineers frequently pair a polarizing filter with cross-polarized illumination, where the light source itself carries a polarizing film oriented at 90 degrees relative to the lens filter. This combination, often called cross-polarization, blocks nearly all specular reflection while permitting the diffusely scattered light carrying genuine surface information to reach the sensor.
A Worked Example: Inspecting Reflective Metal Brackets
Consider a quality control station tasked with detecting hairline scratches on polished stainless steel brackets moving at 40 units per minute. Without any polarization control, the camera captures an image where roughly 70 percent of the bracket surface appears as saturated white pixels due to specular glare from the overhead ring light. The inspection software, unable to distinguish scratch edges from reflection boundaries, produces a false rejection rate of around 12 percent and, worse, misses genuine defects hidden within the glare zones.
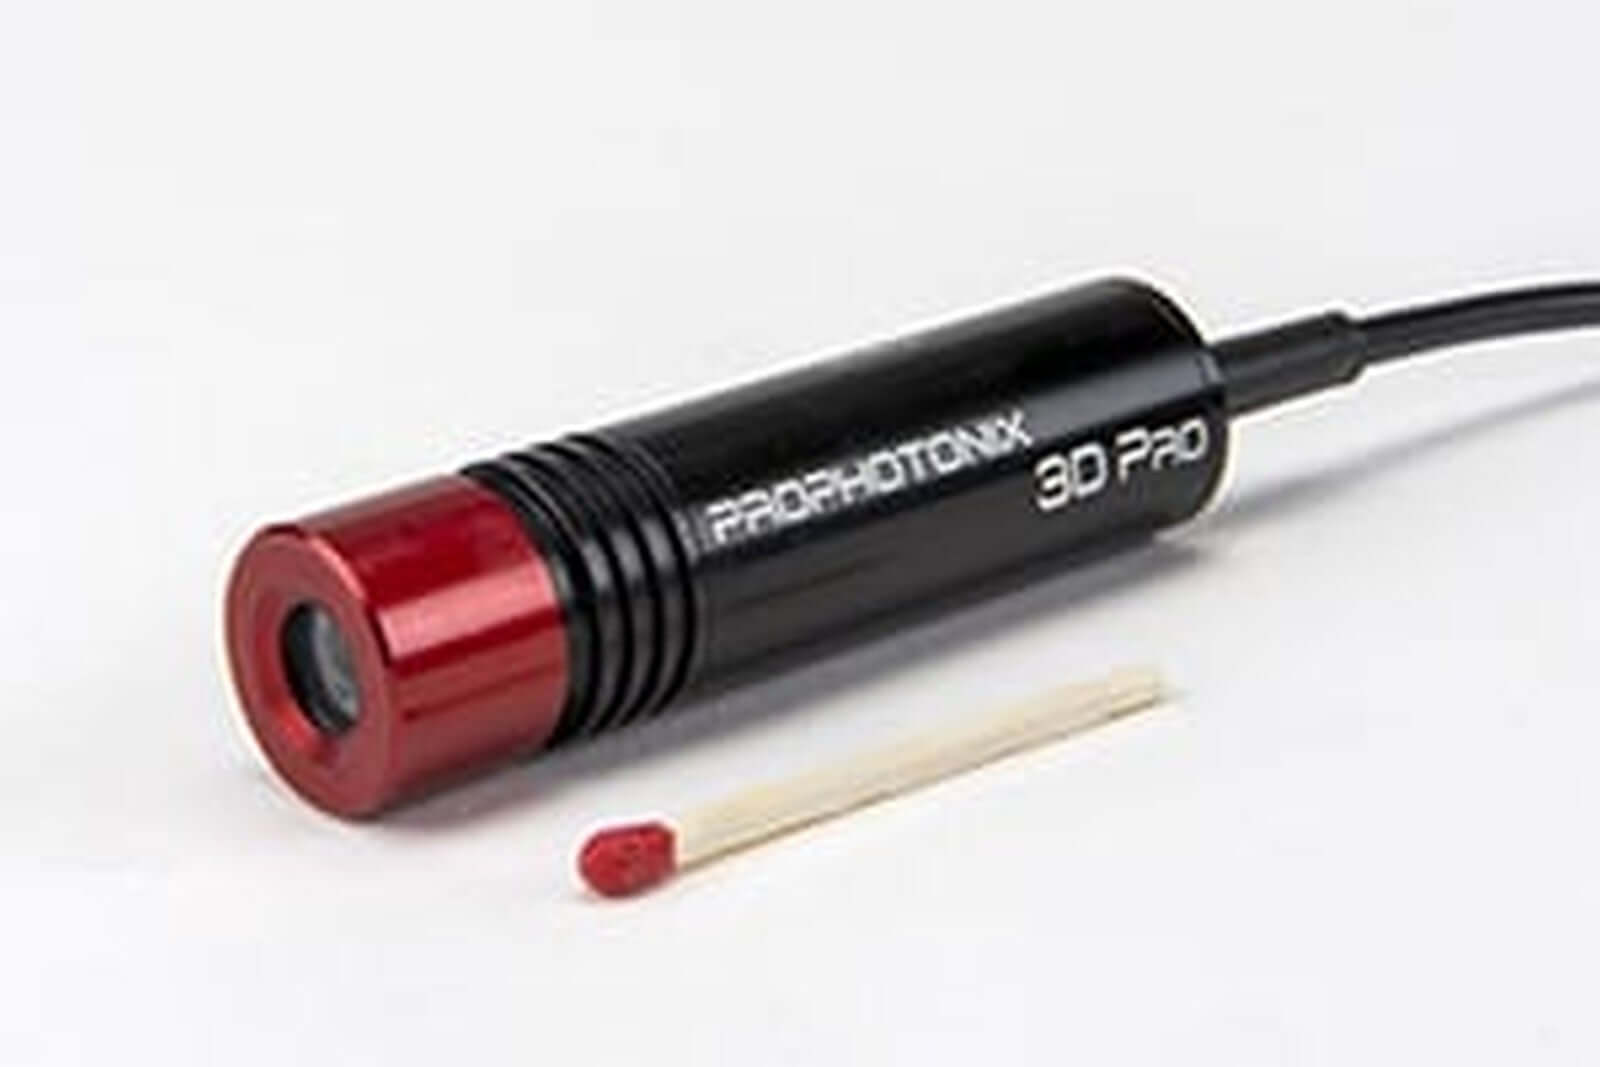
After installing a linear polarization filter on the lens and a matching polarizing sheet over the ring light, oriented at a 90-degree offset, the saturated area drops to under 10 percent of the frame. Surface texture and scratch contrast become visible across nearly the entire bracket. The false rejection rate falls to approximately 2 percent, and the previously undetectable defects in the glare zones become visible and measurable. No change was made to the camera, sensor, or software logic - only the light path was corrected at the optical layer, which is precisely why polarization filters are considered a foundational rather than a supplementary tool in machine vision lens design.
What Are the Trade-Offs Engineers Should Weigh Before Specifying a Filter?
Polarization filters are not a universal fix, and treating them as one leads to disappointing results. On the positive side, they require no changes to camera firmware, software algorithms, or network architecture, which makes them attractive to integrators working within rigid validated systems where recertification of software is costly. They are also passive components with no power draw, no moving parts, and minimal maintenance burden beyond periodic cleaning, which suits the long-duty-cycle environments typical of industrial automation. vision system components
<img src="https://l450v.alamy.com/450v/k373db/me-myself-and-irene-date-2000-k373db.


